Choosing among the top Fiber Marking Laser machines requires more than comparing prices and advertised wattage. Global buyers need reliable marks, stable output, practical software, and responsive technical support. A polished sample can look impressive. Production tells the truth.
Dr. Valentin Gapontsev, the late founder of IPG Photonics, emphasized, “The customer’s application comes first.” This principle remains highly relevant. Stainless steel medical tools, anodized aluminum panels, and black-coated electronics require different marking strategies. Buyers should examine wavelength, pulse duration, beam quality, marking speed, field lens size, and cooling design. A 20-watt source may suit serial numbers, QR codes, and logos. Deeper engraving may require higher power or multiple passes.
Details matter. A clean galvo scanhead can reduce distortion near the marking field’s edges. Stable rotary attachments can improve results on rings, tubes, and cylindrical parts. Easy parameter adjustment also matters when operators change materials during a busy shift. Not every machine performs equally well.
This guide evaluates Fiber Marking Laser machines for international purchasing decisions. It considers machine construction, source reputation, software usability, sample consistency, maintenance access, warranty coverage, and supplier communication. Import requirements and local service availability deserve attention too. A low purchase price may become expensive after delays, replacement parts, or difficult troubleshooting.
No ranking is perfectly universal. That deserves honest reflection. The strongest machine depends on material, production volume, marking depth, factory conditions, and operator skill. Buyers should request test samples using their own parts. They should also verify specifications before ordering. Real evidence beats attractive brochures.
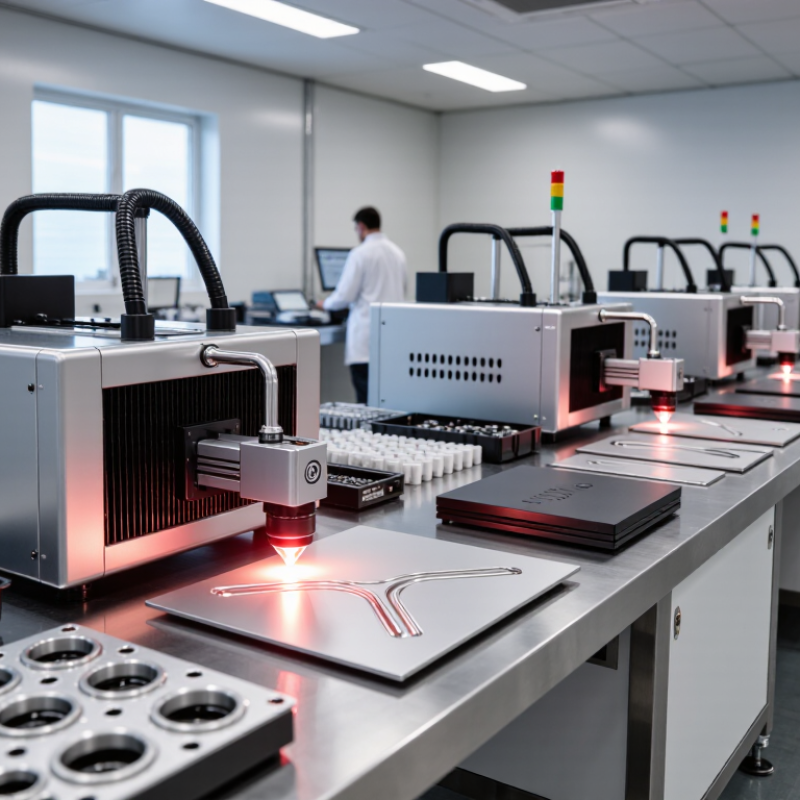
Top Fiber Marking Laser Machines for Global Buyers
Fiber marking systems commonly use a 1064 nm wavelength. This wavelength couples efficiently with stainless steel, aluminum, brass, and coated metals. It can also mark selected engineering plastics after careful testing. In practical workshops, 20 W machines suit serial numbers, logos, and fine text. Their slower speed can still protect small characters from distortion. A 30–50 W class offers a balanced choice for mixed daily work. It handles larger batches and deeper marks with fewer passes.
Higher power changes the workflow. A 60–100 W source can remove coatings faster and produce deeper engraving on suitable metals. However, more power may increase heat, edge spread, or surface discoloration. More power is not automatically better. Lens selection, scan speed, pulse frequency, and focal accuracy affect the result just as much. A 160 mm lens may cover a broad area, while a shorter lens can produce finer detail. Operators should inspect the focus point on every new material.
From hands-on trials, identical settings rarely perform identically across different alloys. I still recheck contrast after cleaning, because oil residue can mislead the first sample. A reliable buyer should request test marks, measured cycle times, and maintenance requirements. Enclosed systems also need suitable extraction, interlocks, and documented operator training. Regional electrical standards and workplace rules deserve verification before purchase. Small details matter.
Fiber Marking Fundamentals: 1064 nm Wavelength and 20–100 W Power Classes
This chart compares commonly specified continuous-wave fiber marking laser power classes operating around the 1064 nm wavelength. Lower-power systems are widely used for general metal marking, while higher-power classes can support faster processing, deeper engraving, and more demanding production workloads. Actual results depend on material, lens, scan head, pulse settings, and part geometry.
Speed and spot size shape real marking quality. Some fiber systems advertise speeds up to 7,000 mm/s. However, production speed is usually lower. Hatch spacing, lens choice, focus accuracy, and material response all matter. A small stainless-steel code may finish quickly, while deep annealing needs slower passes.
Spot sizes between 10 and 30 μm support fine text, serial numbers, and dense Data Matrix codes. Smaller spots can improve edge definition, but they also demand accurate focusing. ISO 11145:2018 provides standard terminology for laser beam parameters. ISO 11554 also guides optical power measurement. Buyers should request measured test results, not only catalogue claims. MarketsandMarkets’ 2024 Laser Marking Market report identifies traceability and automated manufacturing as major demand drivers. That supports investment, but it does not guarantee equal performance across materials.
Tips: Ask for a sample mark on your actual alloy or plastic. Measure contrast, depth, cycle time, and code readability. Test at several speeds. A 7,000 mm/s setting may look impressive, yet it can produce weak contrast or uneven lines. I have seen specifications hide the hardest detail: whether speed refers to galvo travel or completed marking. That difference deserves careful review. Include lens focal length, spot measurement method, power stability, and software controls in the comparison. Performance claims should be repeatable.
For global buyers, fiber marking lasers should be compared by material response, not only by wattage. Q-switched fiber lasers remain practical for stainless steel, aluminum, brass, and coated metals. Their short, high-energy pulses create crisp serial numbers and logos at a competitive cost. They are reliable workhorses. However, their fixed pulse behavior can produce excess heat on thin parts or sensitive coatings.
MOPA fiber lasers offer adjustable pulse width and finer process control. This helps create dark marks on anodized aluminum, cleaner results on plastics, and controlled color effects on selected metals. In production trials, I would inspect edge quality under magnification, not trust visual contrast alone. A mark may look sharp but fade after abrasion testing. That detail is easy to miss.
UV-converted fiber lasers operate at a shorter wavelength, commonly near 355 nm. They transfer less heat into many plastics, glass surfaces, films, and miniature electronic components. Their smaller heat-affected area benefits delicate parts, though the initial investment and maintenance demands are usually higher. Test samples should match real production conditions, including curved surfaces, dust, humidity, and repeated shifts. No machine fits every factory. A technically sound choice can still fail when software, extraction, or operator training is overlooked.
Top Fiber Marking Laser Machines for Global Buyers
Global buyers should treat compliance as a purchasing test, not a paperwork exercise. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023. That growth increases demand for stable, traceable marking systems. CE compliance should include the correct technical file, risk assessment, declaration of conformity, and machine labeling. CE is not a quality award. It confirms applicable European requirements were assessed.
IEC 60825-1 defines laser safety classes, accessible emissions, warning labels, and protective controls. A fiber marker may require enclosure interlocks, emergency stops, beam shielding, and controlled access. UL certification can support North American acceptance, but buyers should verify the exact standard and certification scope. A supplier’s general electrical certificate may not cover the complete machine. That detail is often missed.
IP-rated enclosures require equal attention. Under IEC 60529, IP54 indicates limited dust ingress and protection against water spray. It does not prove laser safety, cooling performance, or resistance to metal dust. The European Commission’s Safety Gate 2023 report recorded 3,412 product alerts, showing why documented conformity matters. During audits, I would inspect test reports, serial-number links, labels, interlock checks, and maintenance records. A clean enclosure can still conceal weak engineering. Documents can also be outdated. Buyers should request current evidence for the delivered configuration.
Choosing a fiber marking laser starts with the material, not the advertised wattage. Bare stainless steel, aluminum, brass, and coated plastics react differently to heat. In production trials, inspect contrast, edge sharpness, and heat tint. Stainless steel often suits crisp annealed marks, while aluminum may need controlled power. Plastics require caution; some melt, smoke, or lose contrast quickly. Test real parts, not polished samples. That detail matters.
Batch volume changes the buying decision. A workshop marking 200 parts weekly may value simple setup over maximum speed. A supplier processing 20,000 housings needs repeatable positioning, barcode verification, and efficient fixtures. Cycle time includes loading, focusing, inspection, and rework. A fast scan head cannot rescue slow handling. Keep samples from several shifts. Operators reveal problems engineers miss.
For ROI, record labor minutes, rejected parts, consumables, maintenance, and downtime. Divide the investment by realistic monthly savings, not optimistic brochure figures. A spreadsheet helps, but it can still mislead. I once underestimated fixture changes and overstated the payback estimate. That mistake was useful. Request a production test using your materials, artwork, and target volume. Confirm mark durability after cleaning, abrasion, or heat exposure. Reliable decisions come from measured trials and honest assumptions.